Home
Multi-layer Co-extruded Barrier FilmThermoforming Barrier SheetVacuum & Retort Barrier FilmHigh-Barrier Lidding FilmVacuum Skin Packaging FilmFFS & Form-Fill-Seal Roll FilmLamination & Barrier FilmEVOH Barrier ResinVacuum Pouches & Barrier BagsShrink Bags & FilmsStand-Up PouchesIBC & FIBC LinersCIPP Liner FoilAll products →Applications →
ApplicationsAbout
BlogNewsKnowledgeDownloadsTechnical DataAll resources →
FAQContact
Non-Food packaging

Medical & Pharmaceutical

Sterile barrier packaging has one job: keep the product sterile and prove it. The material and seal are selected against the sterilisation method and the agreed specification.

01

What goes wrong

Documented failure modes
Failure modes

Sterile barrier integrity must survive distribution abuse

Traceability to every lot is a regulatory requirement

Ethylene oxide or gamma sterilisation compatibility

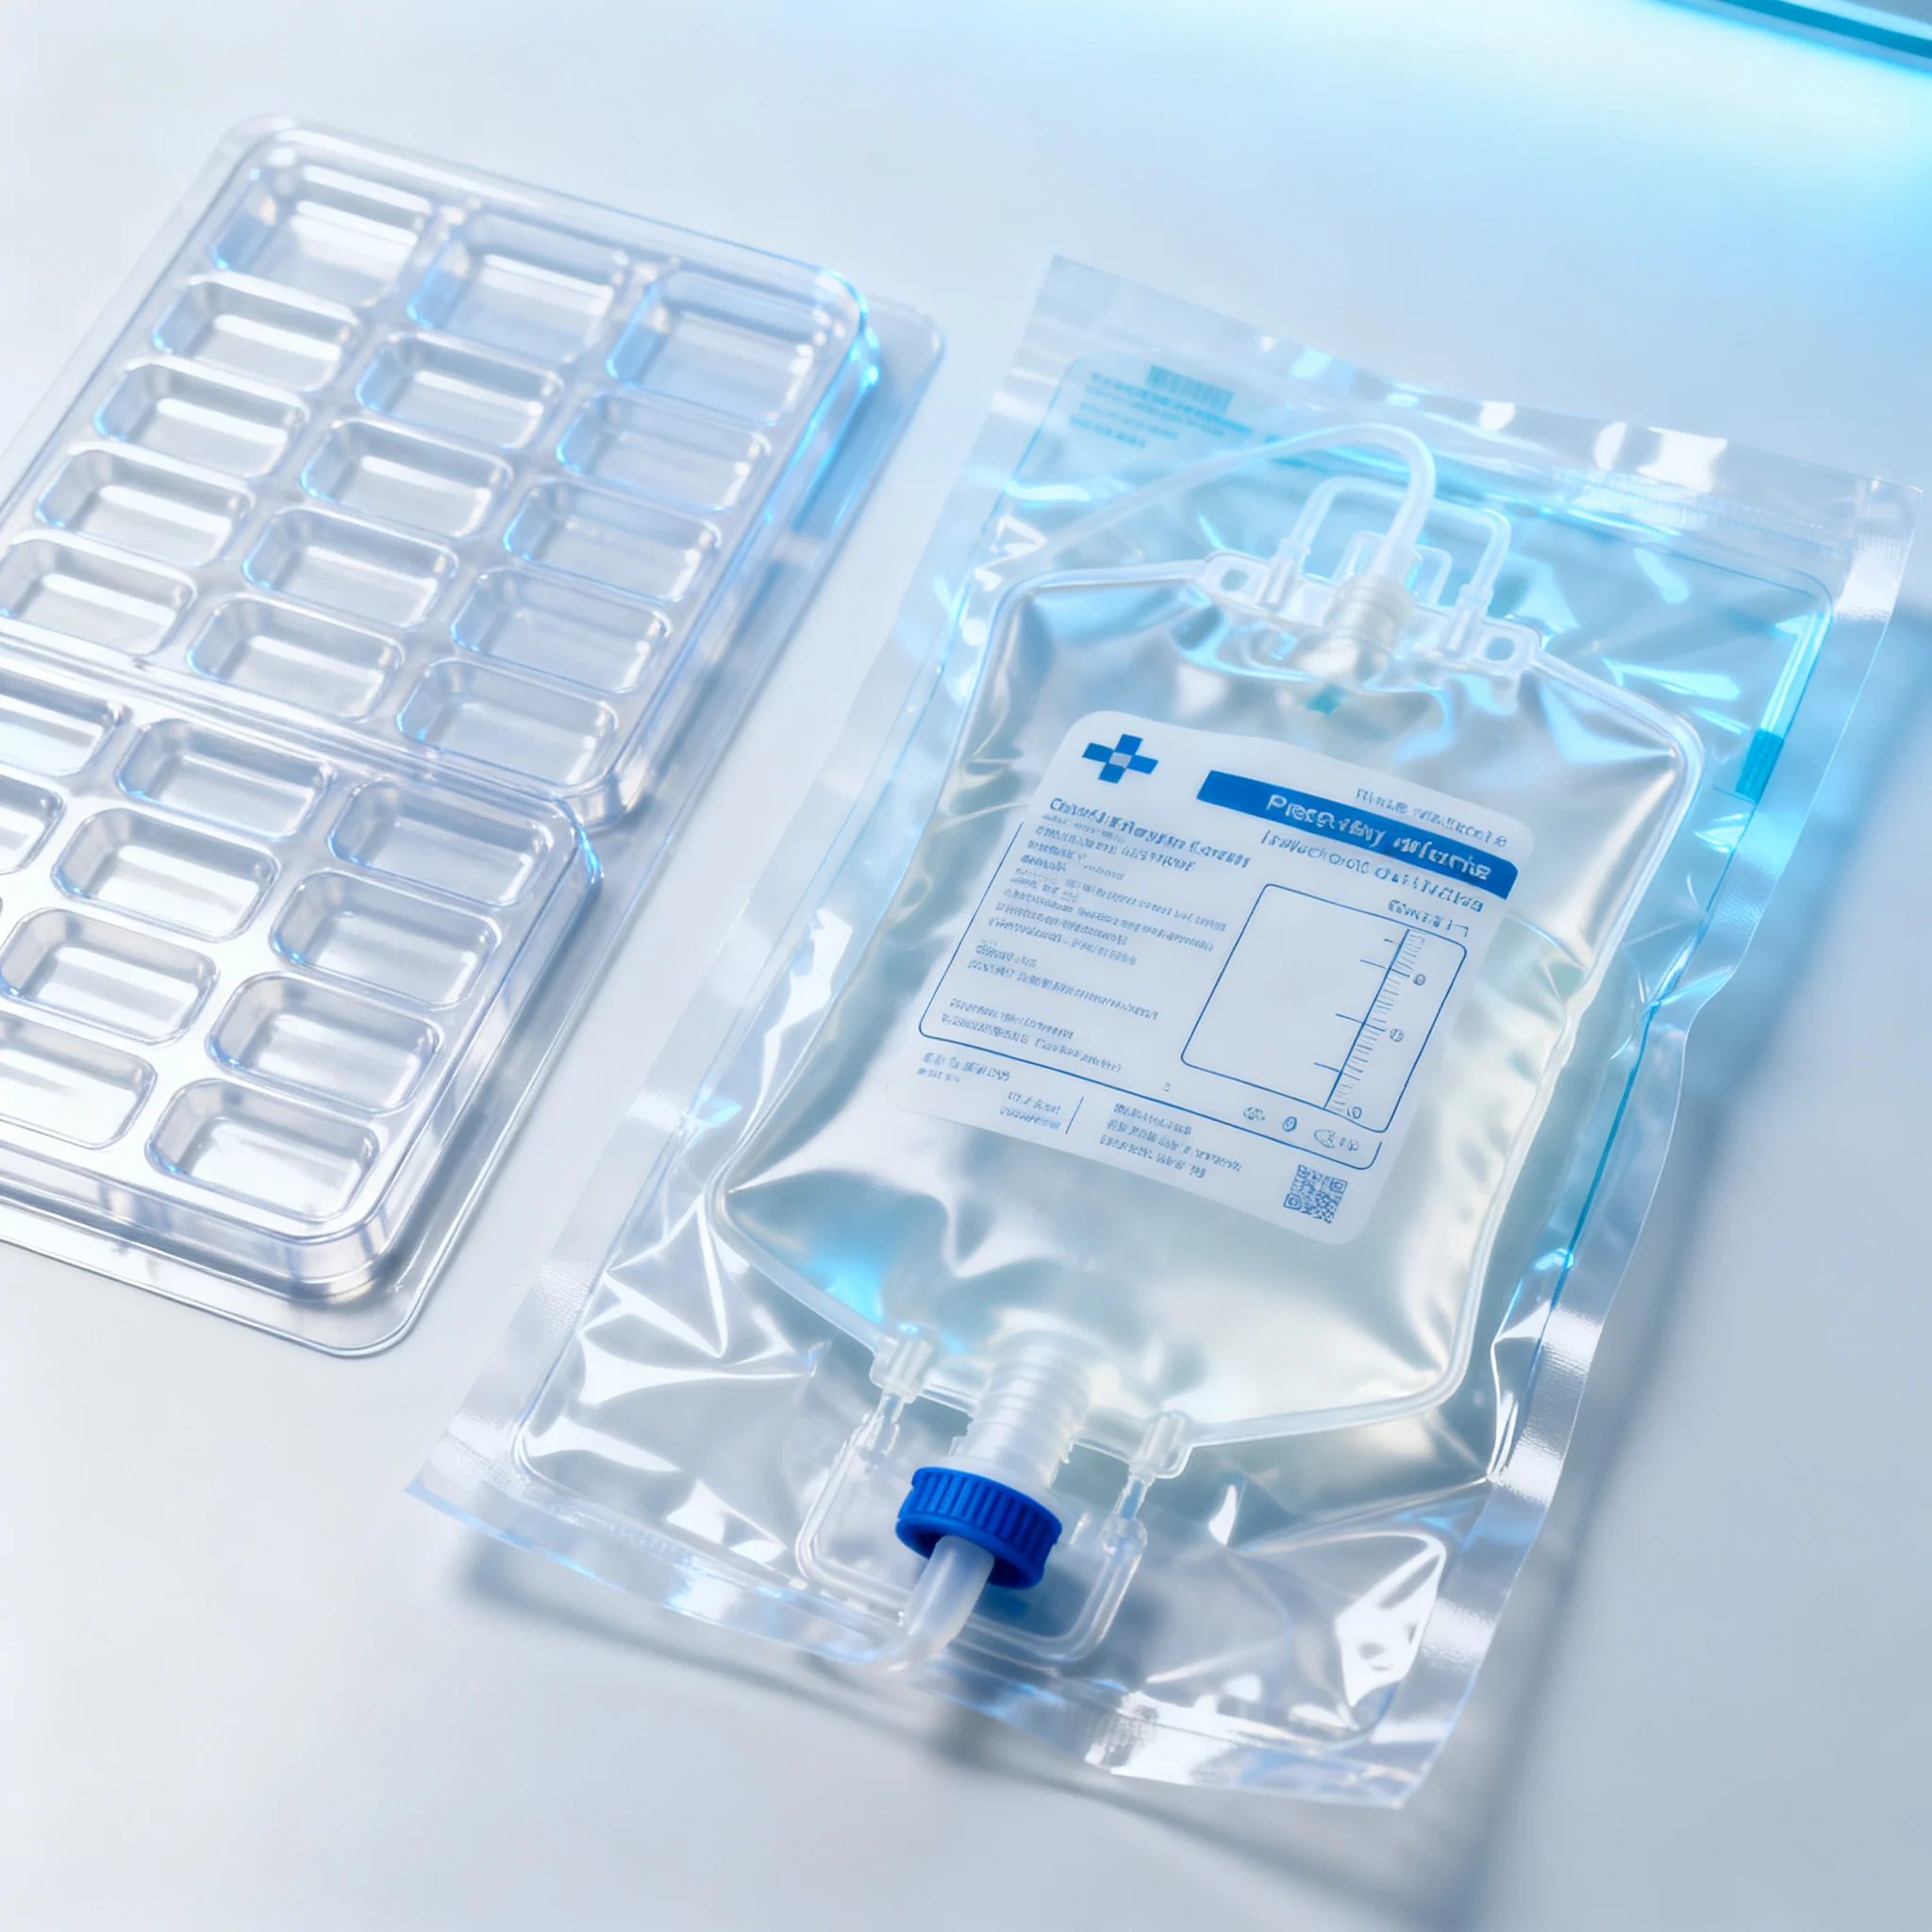
Infusion bags need 121 °C steam sterilisation

Failure modes / 4 documentedStart with the failure, not the film.
02

How the structure fixes it

Engineering response

Validated barrier structures with documented OTR values

Lot-level identification to be confirmed at order stage

Grades compatible with EtO, gamma and steam sterilisation

Secondary packaging for infusion bags validated to 121 °C

Response / structure + gauge + barrierEvery layer earns its place.
EtO / gamma / steam
Sterilisation
121 °C
Steam
Lot-level
Traceability
Medical & Pharmaceutical
Recommended products

Structures specified for medical & pharmaceutical

Specifying for medical & pharmaceutical?

Tell us the product and the shelf life you need to hit. We will propose a structure and put a sample in front of you.